What Industrial Machinery Manufacturers Need From a Computer
Industrial machinery manufacturers build, integrate and support equipment that runs in factories, workshops, clean rooms and outdoor enclosures — CNC machines, packaging lines, textile equipment, injection moulding systems, automated test rigs, laser markers and material handling systems. Every one of those machines needs at least one computer to run the HMI, collect sensor data, talk to PLCs, log production data or serve as the operator console. The requirements are very different from an office desktop: continuous operation, tolerance of dust and vibration, wide temperature range, stable long-term supply and a predictable operating system image.
The Technical Specification That Matters
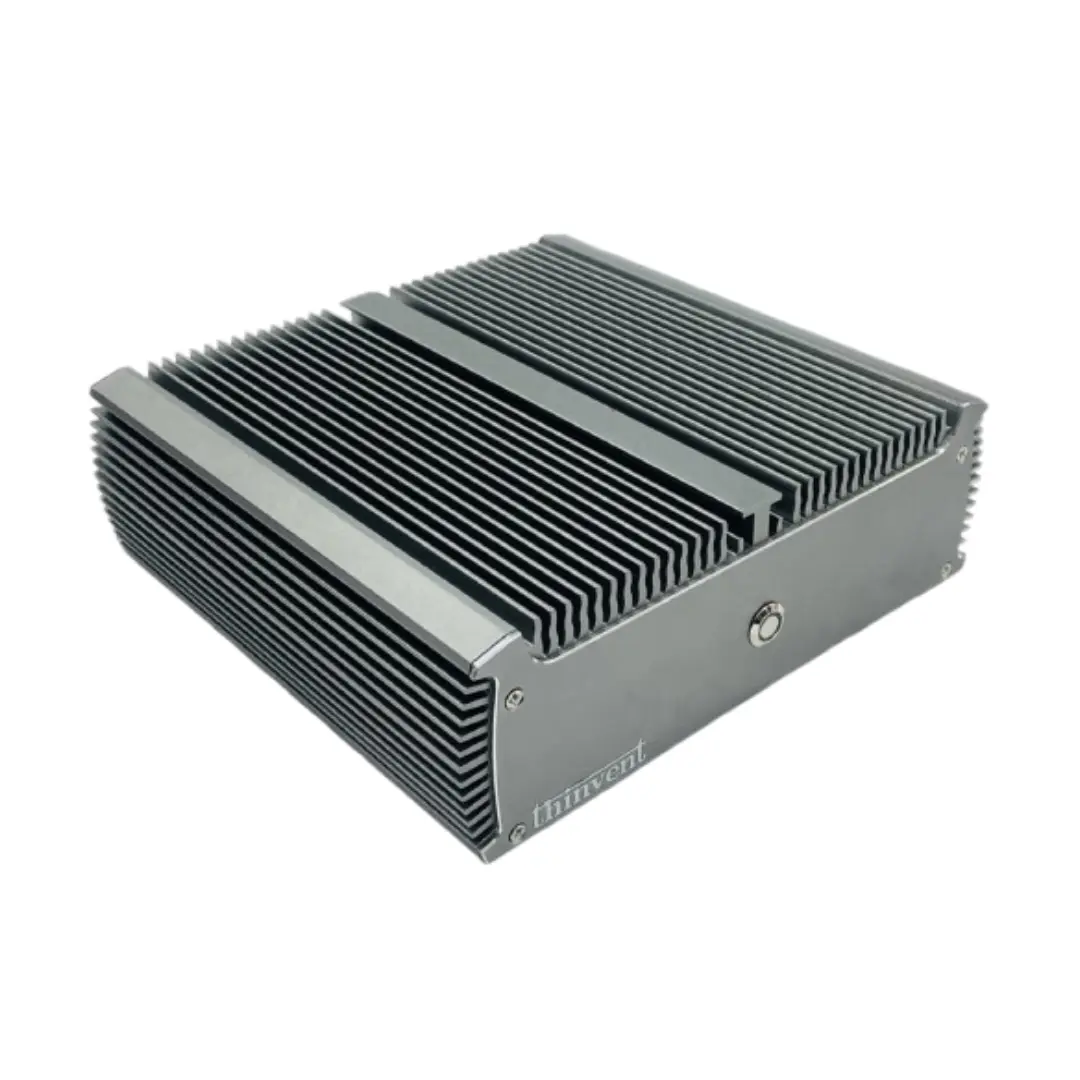
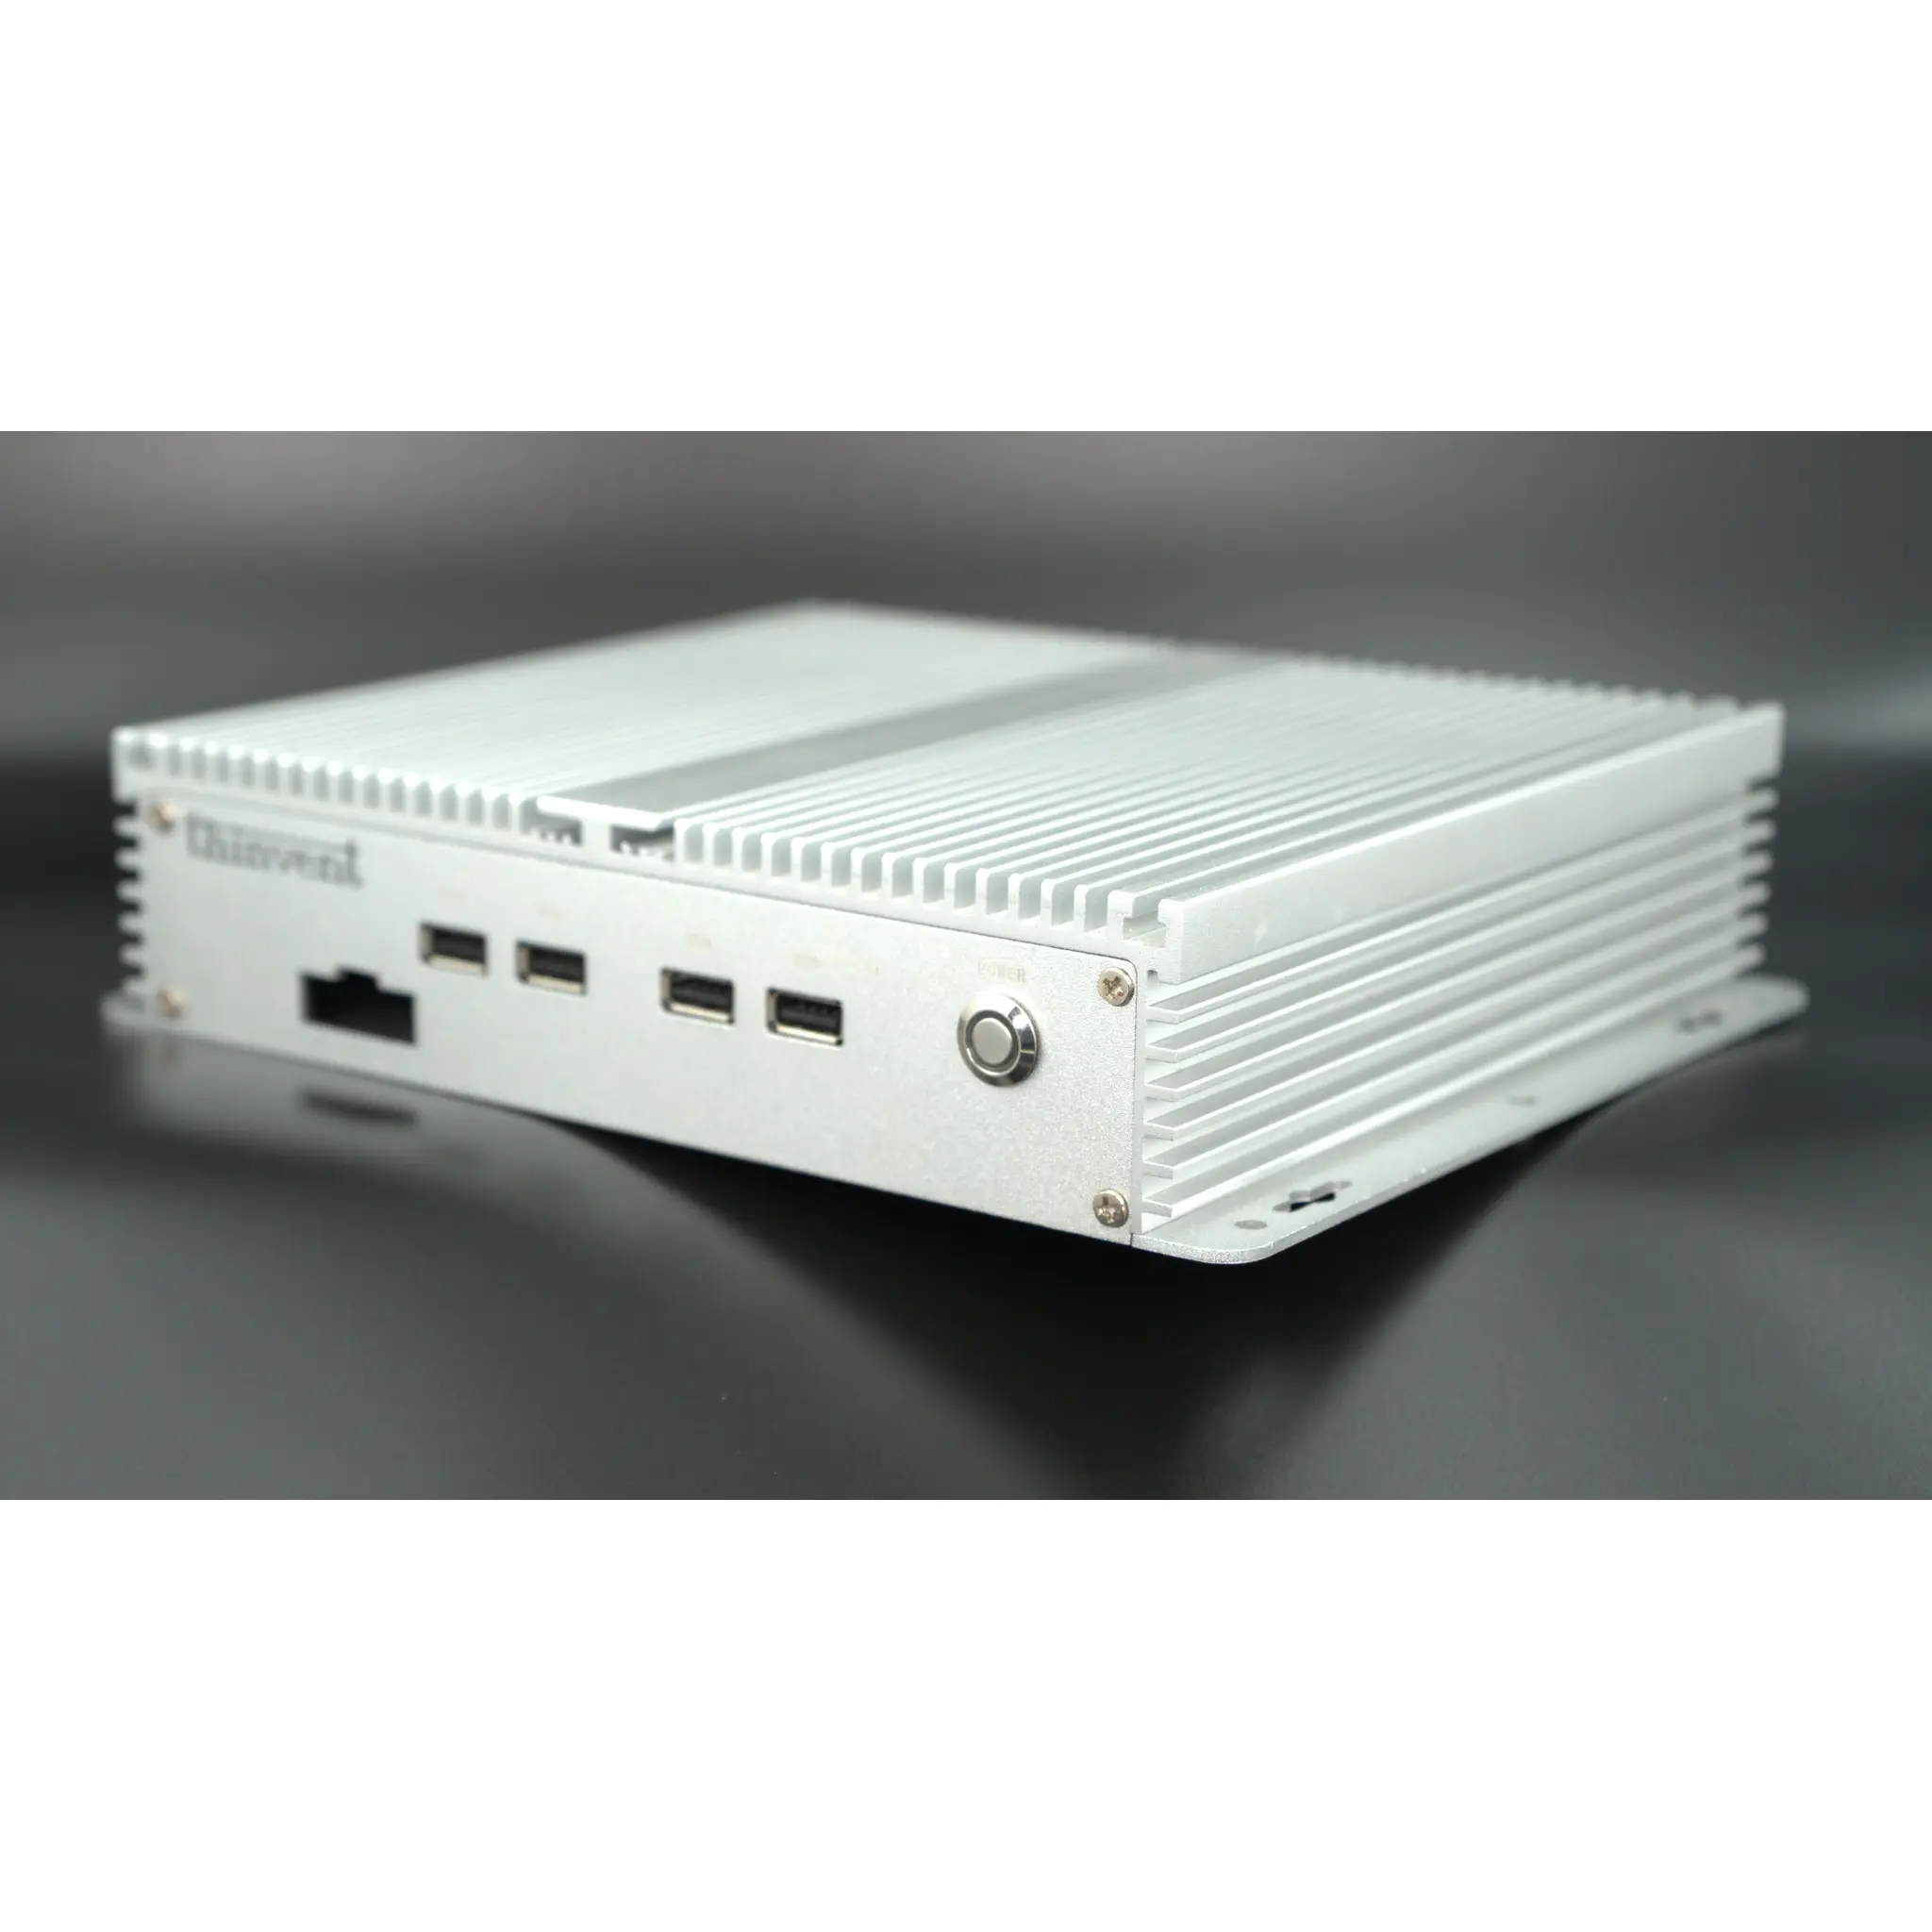
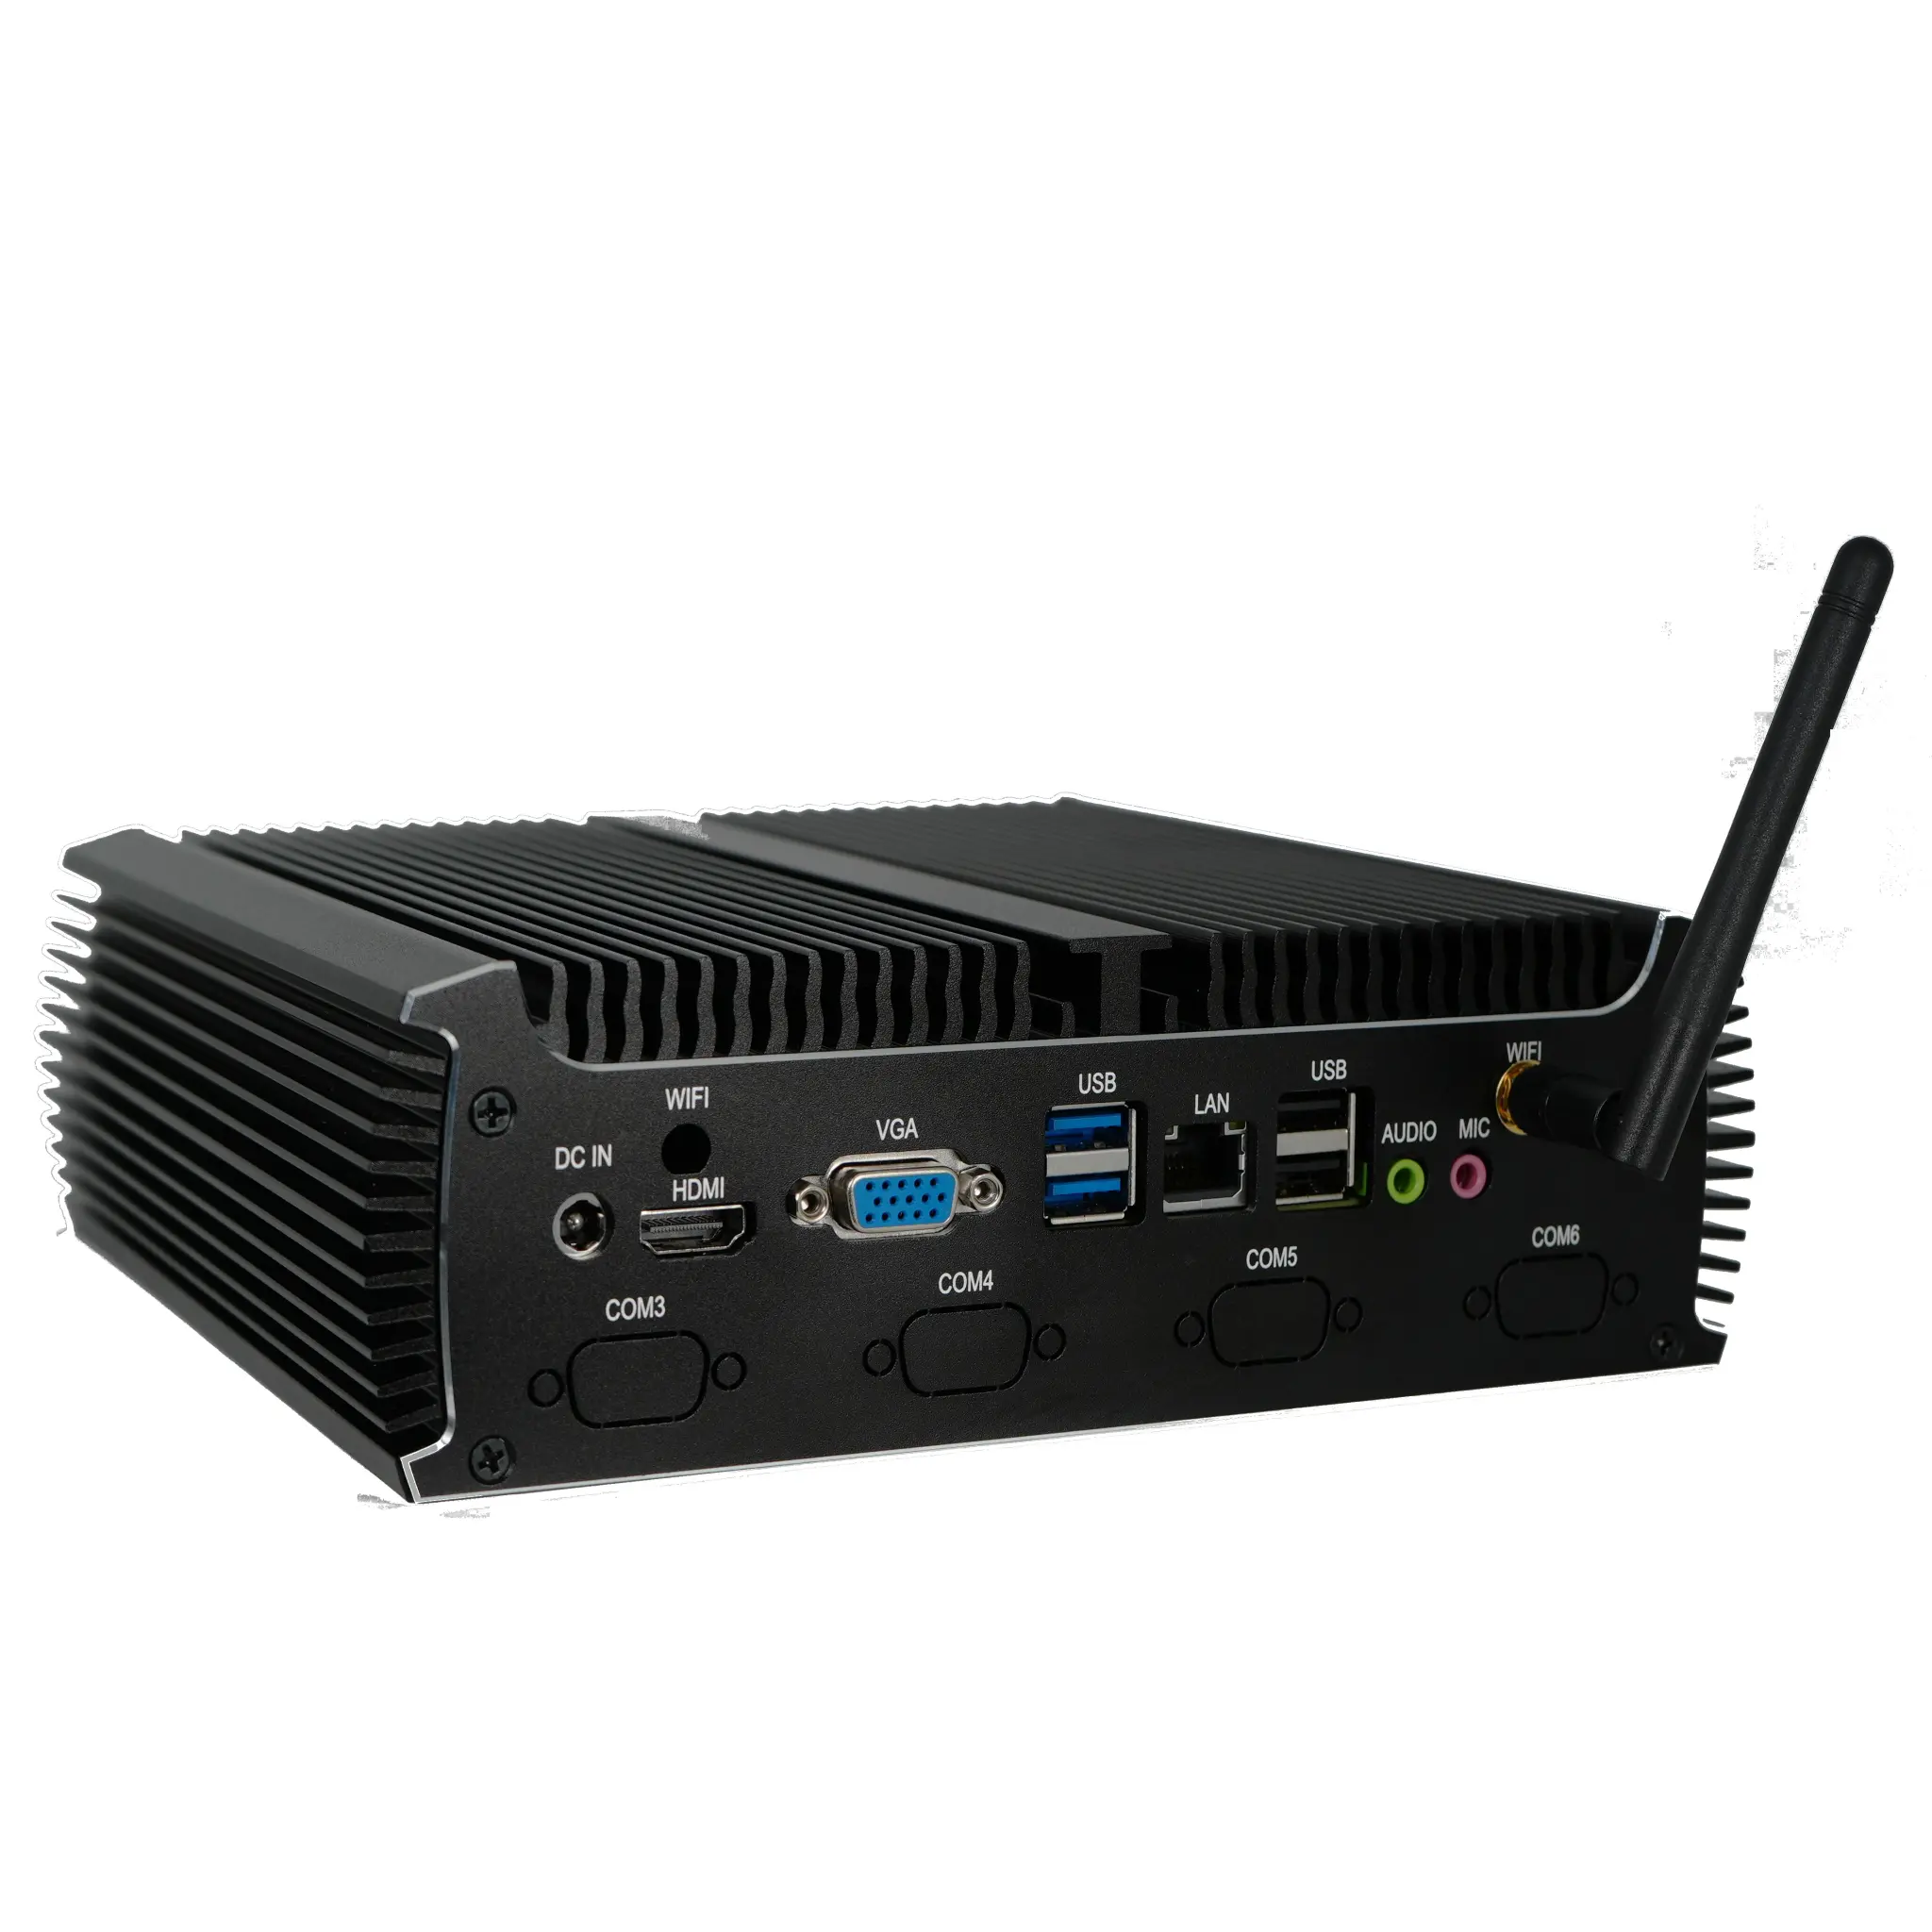
The typical control-cabinet computer is a fanless industrial PC with a solid-state drive, no rotating parts, and a DC input that matches the panel supply (commonly 12 V or 24 V). Fanless designs matter because a fan pulls conductive dust and metal filings straight into the chassis. Beyond that, engineers usually care about serial connectivity for legacy equipment, dual Gigabit Ethernet for separating the machine network from the plant network, and watchdog timers or auto power-on so the machine restarts itself after a power interruption. Cores and memory are chosen for the workload: 4-core processors handle HMI, kiosk and data-logging duty comfortably, while 6- to 12-core CPUs make sense when the same box also runs vision, edge analytics or a local database.
| Requirement | Typical Industrial Choice | Why |
|---|---|---|
| Cooling | Fanless, aluminium heatsink chassis | Dust, filings and vibration kill fans |
| Storage | SSD 128 GB – 1024 GB | No moving parts, faster boot after power loss |
| Serial I/O | RS-232 / RS-485 ports | Legacy PLCs, drives, weighing scales |
| Networking | Dual Gigabit Ethernet | Separate machine and plant networks |
| Power | 12 V or 24 V DC input | Runs from the panel supply |
| Operating system | Windows 11 Pro, Windows 11 IoT, Ubuntu, Embedded Linux | Long support windows and image control |
| Mounting | DIN rail, VESA or panel mount | Fits inside the control cabinet |
Common Applications on the Factory Floor
Industrial machinery builders typically deploy these systems in five roles. Operator HMI panels replace fragile consumer tablets on the shop floor. Machine gateways poll PLCs over Modbus or OPC UA and push data to MES or SCADA. Vision and inspection stations need more compute and dual-display output. Kiosk and terminal stations at the machine feed material issue, job cards or quality checks. Test and burn-in benches run long unattended scripts where the computer must never sleep or throttle. In all five cases, the buyer is looking for a supplier who can hold the same specification for years, supply spare units, and pre-load a locked-down OS image.
What to Look For in a Supplier
When evaluating industrial computer suppliers for machinery integration, ask four questions: can they supply a fanless design with DC input rather than an ATX board in a box; do they offer serial and dual-Ethernet options without a custom redesign; can they ship the same board revision over a multi-year machine programme; and do they support Windows IoT, Linux and no-OS builds from one hardware platform? A supplier who answers yes