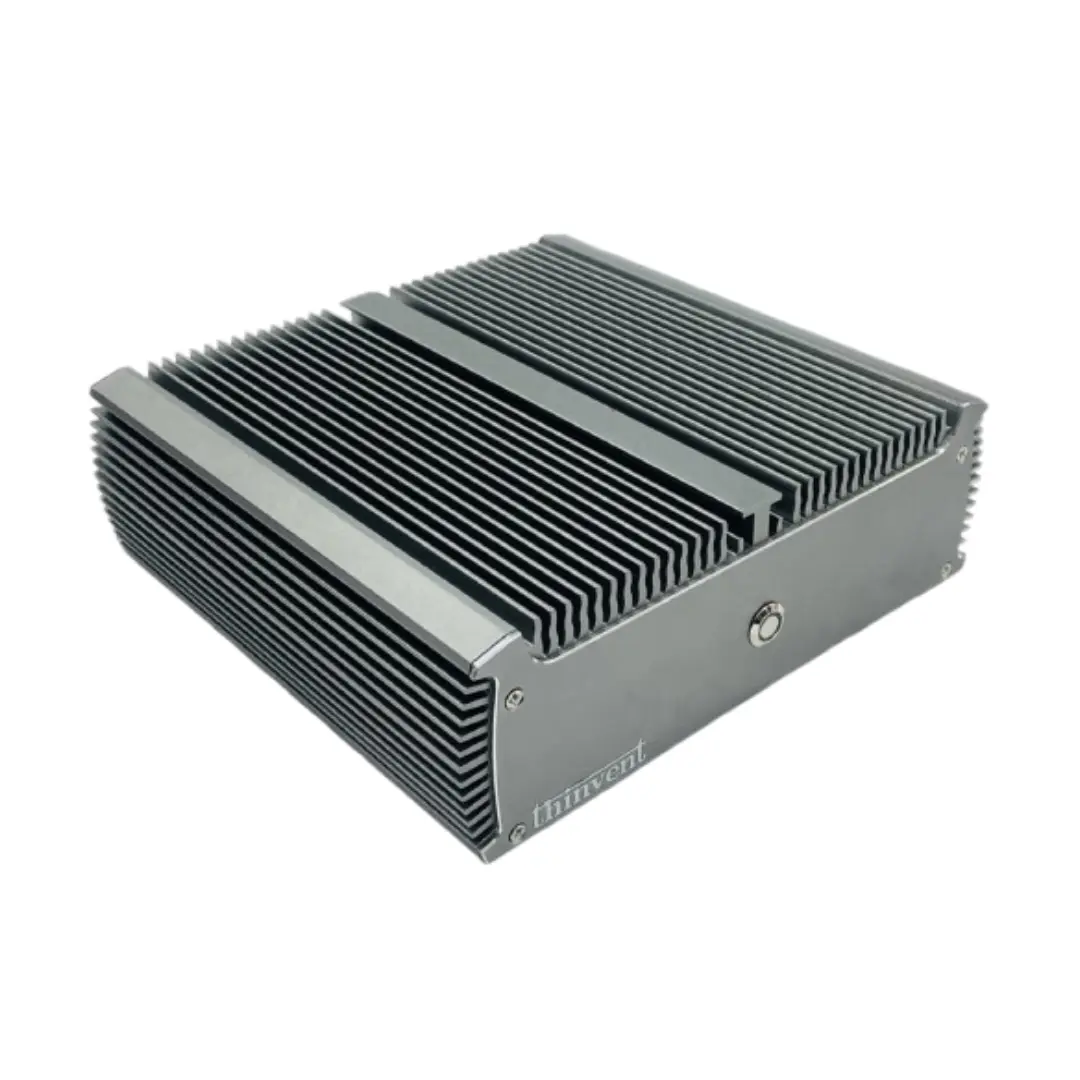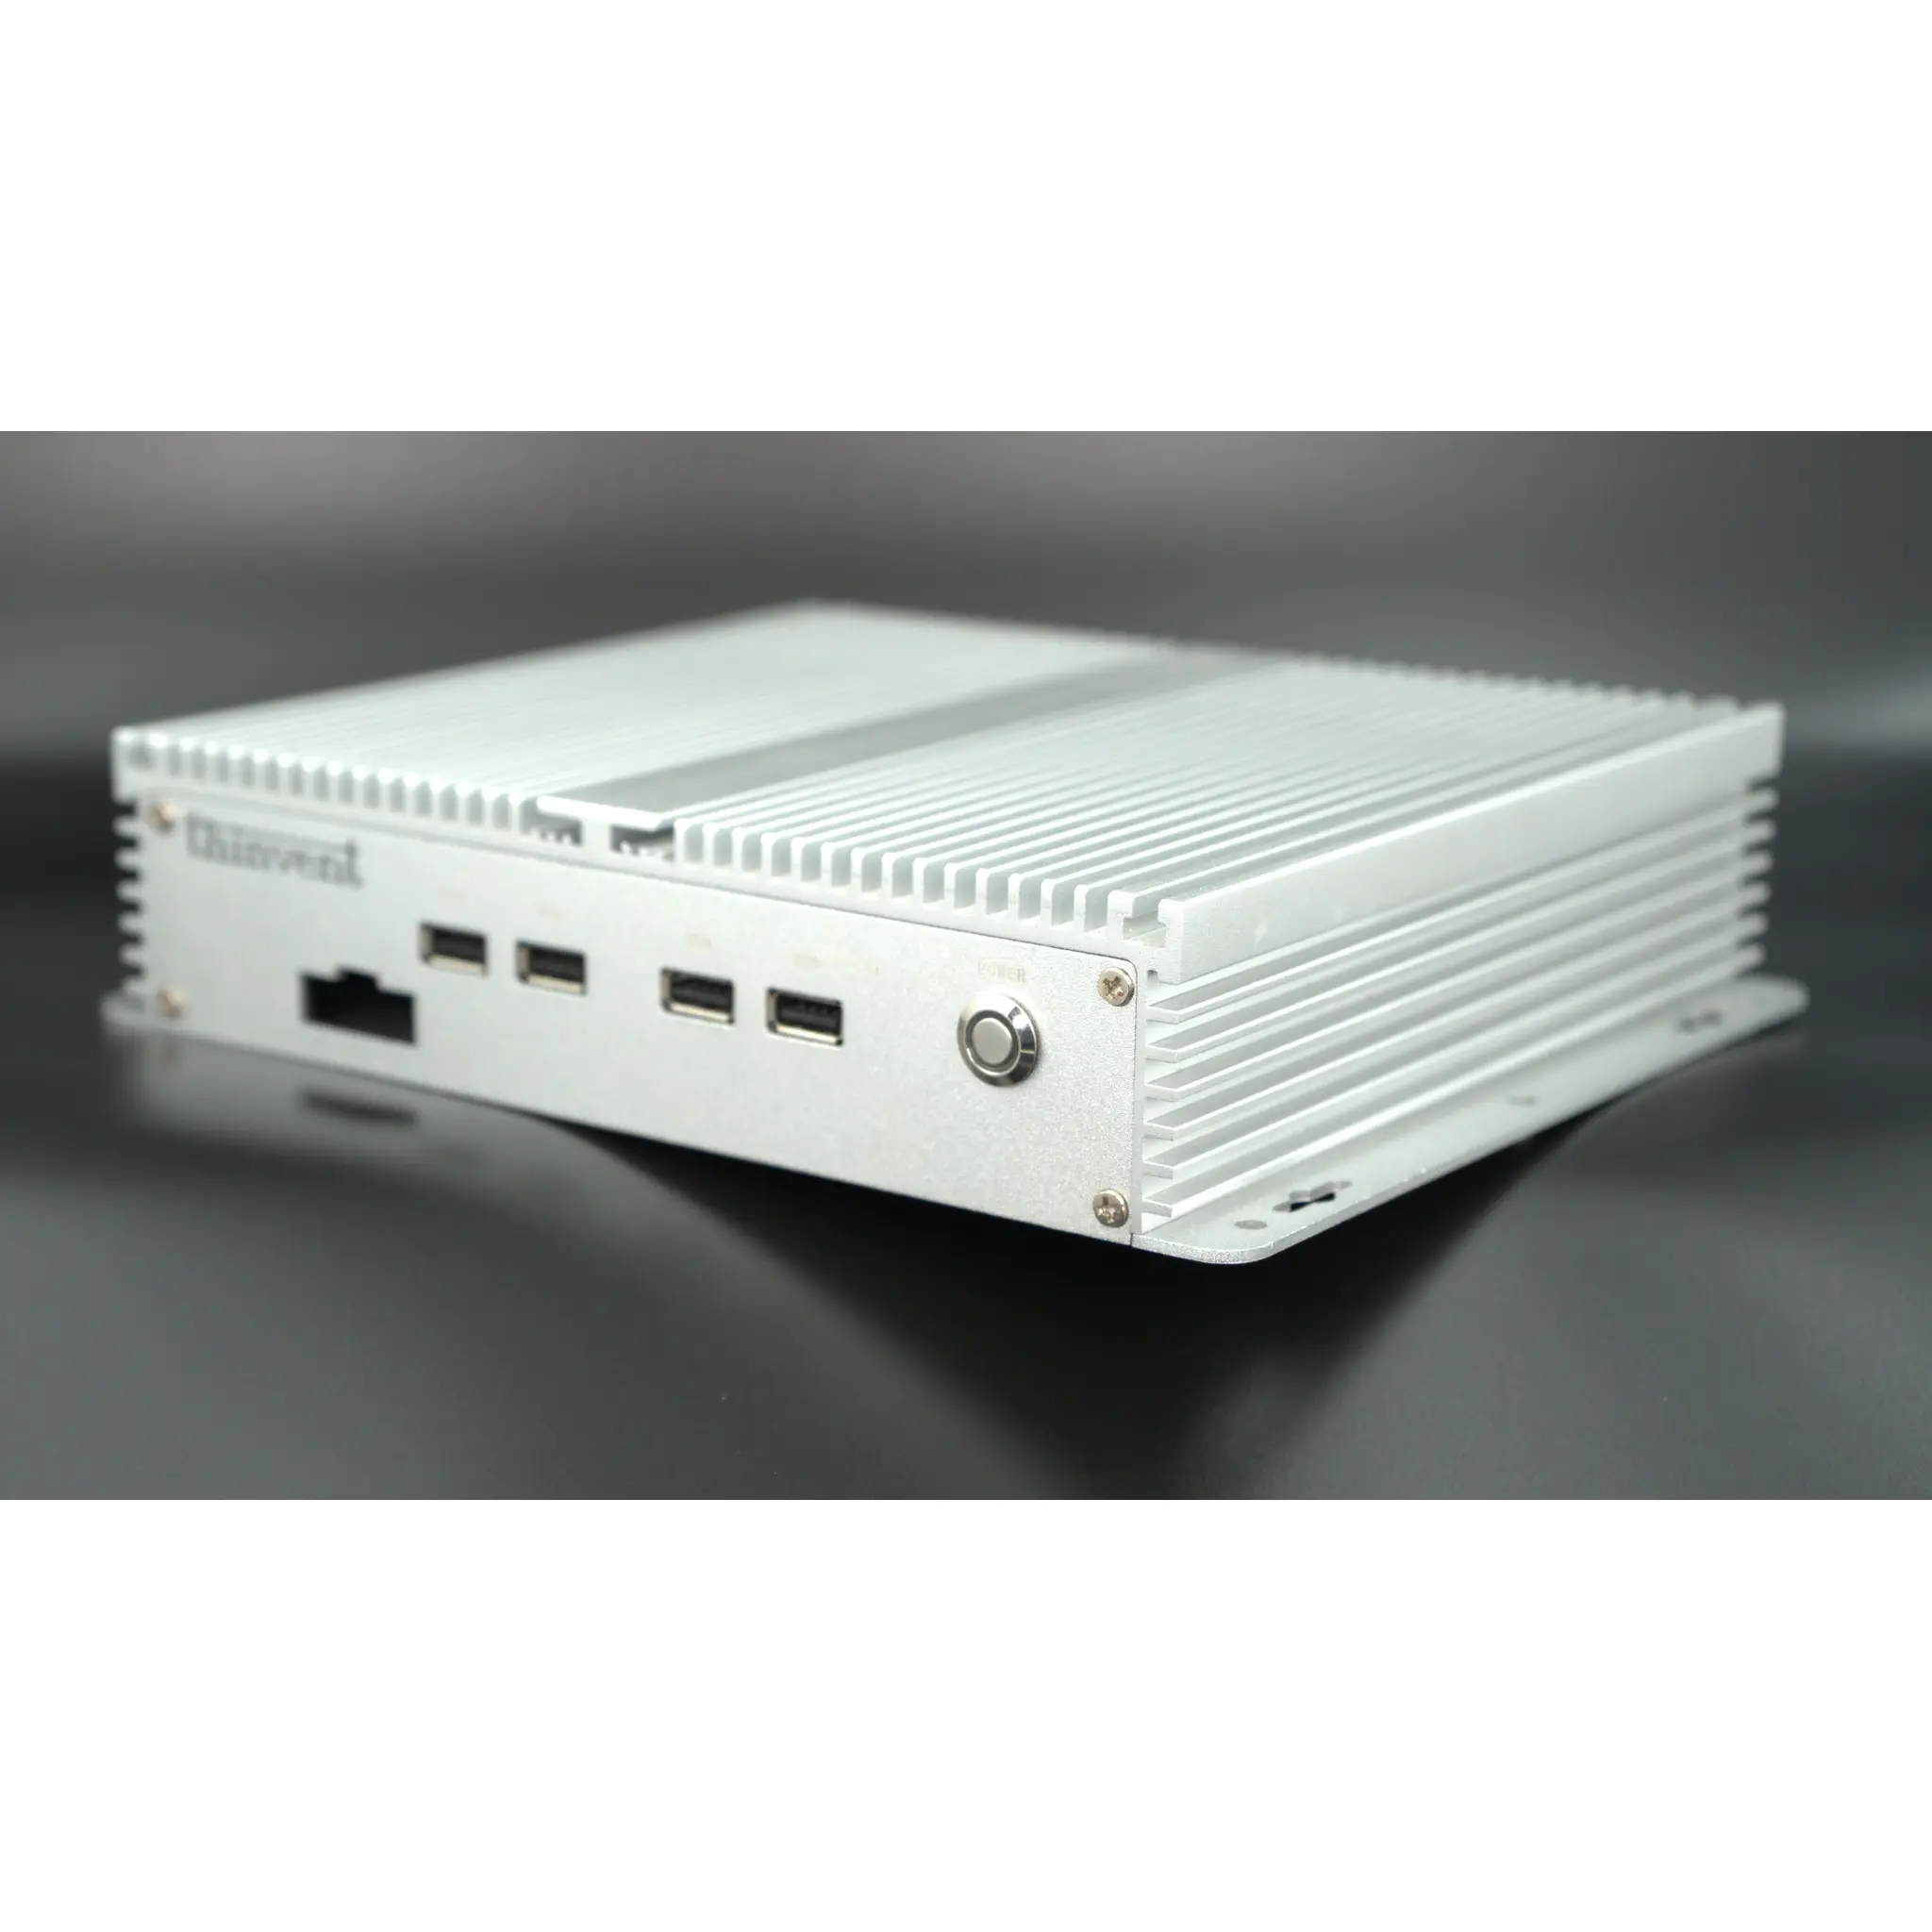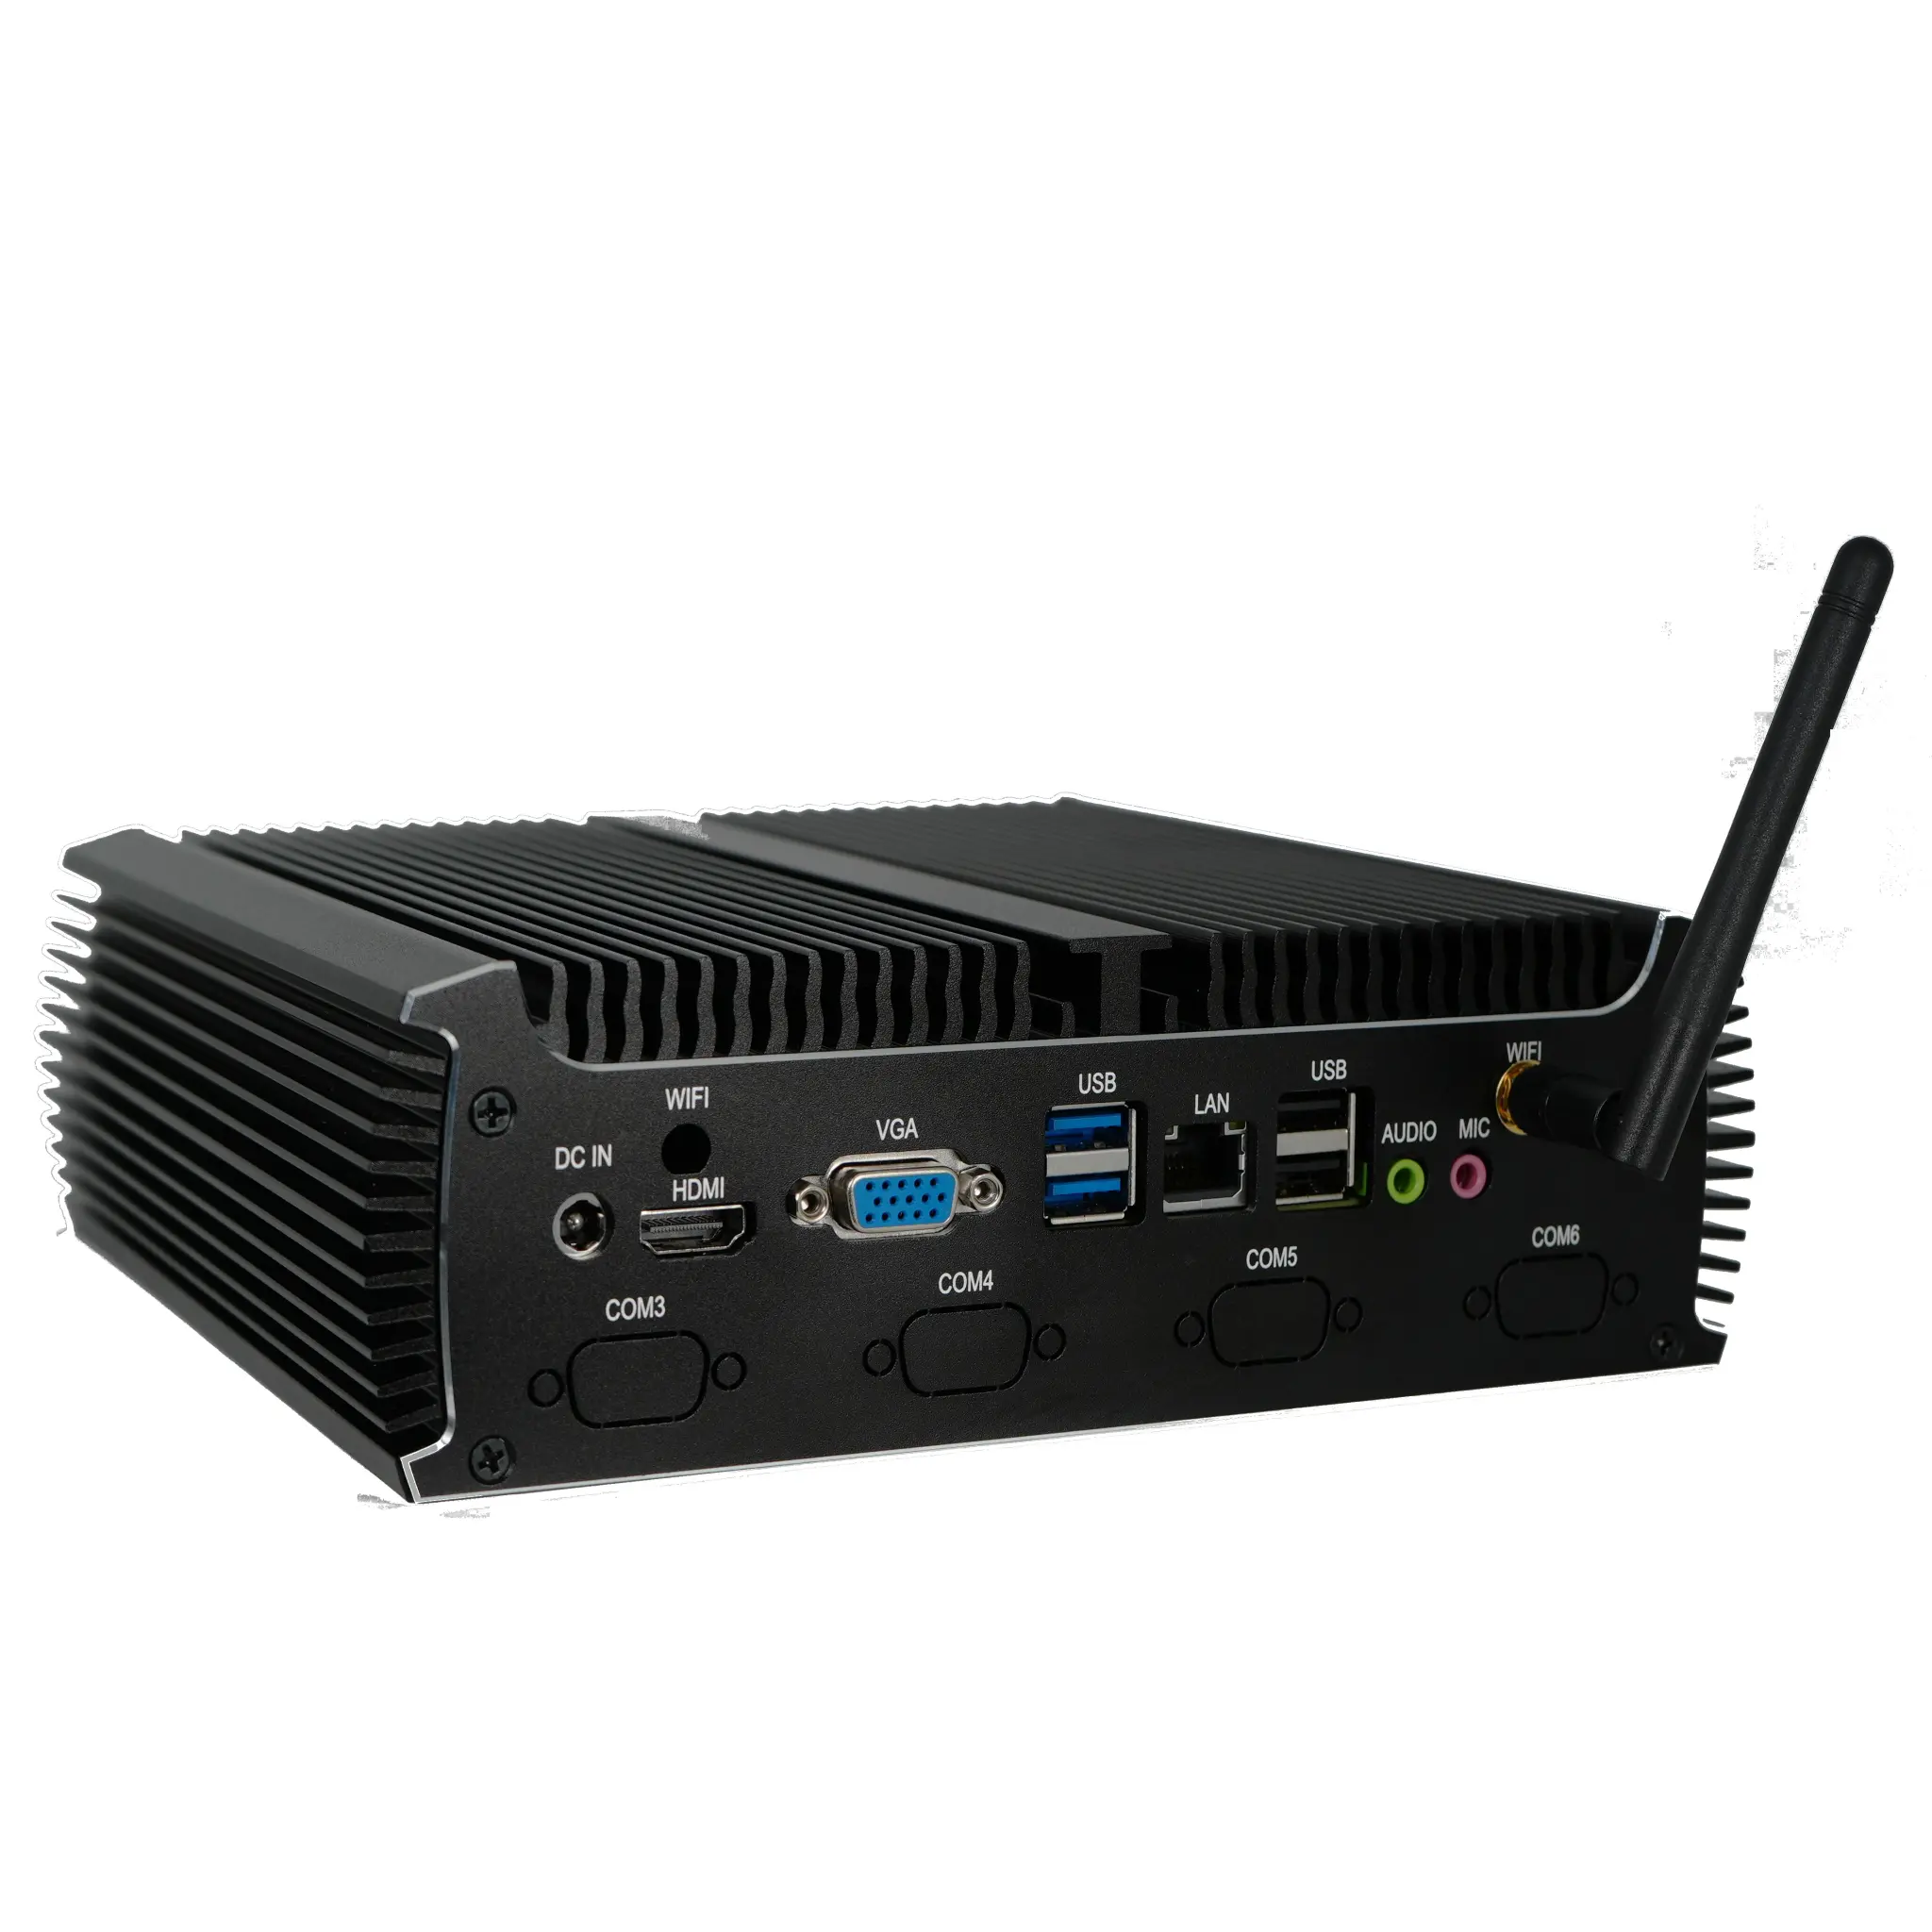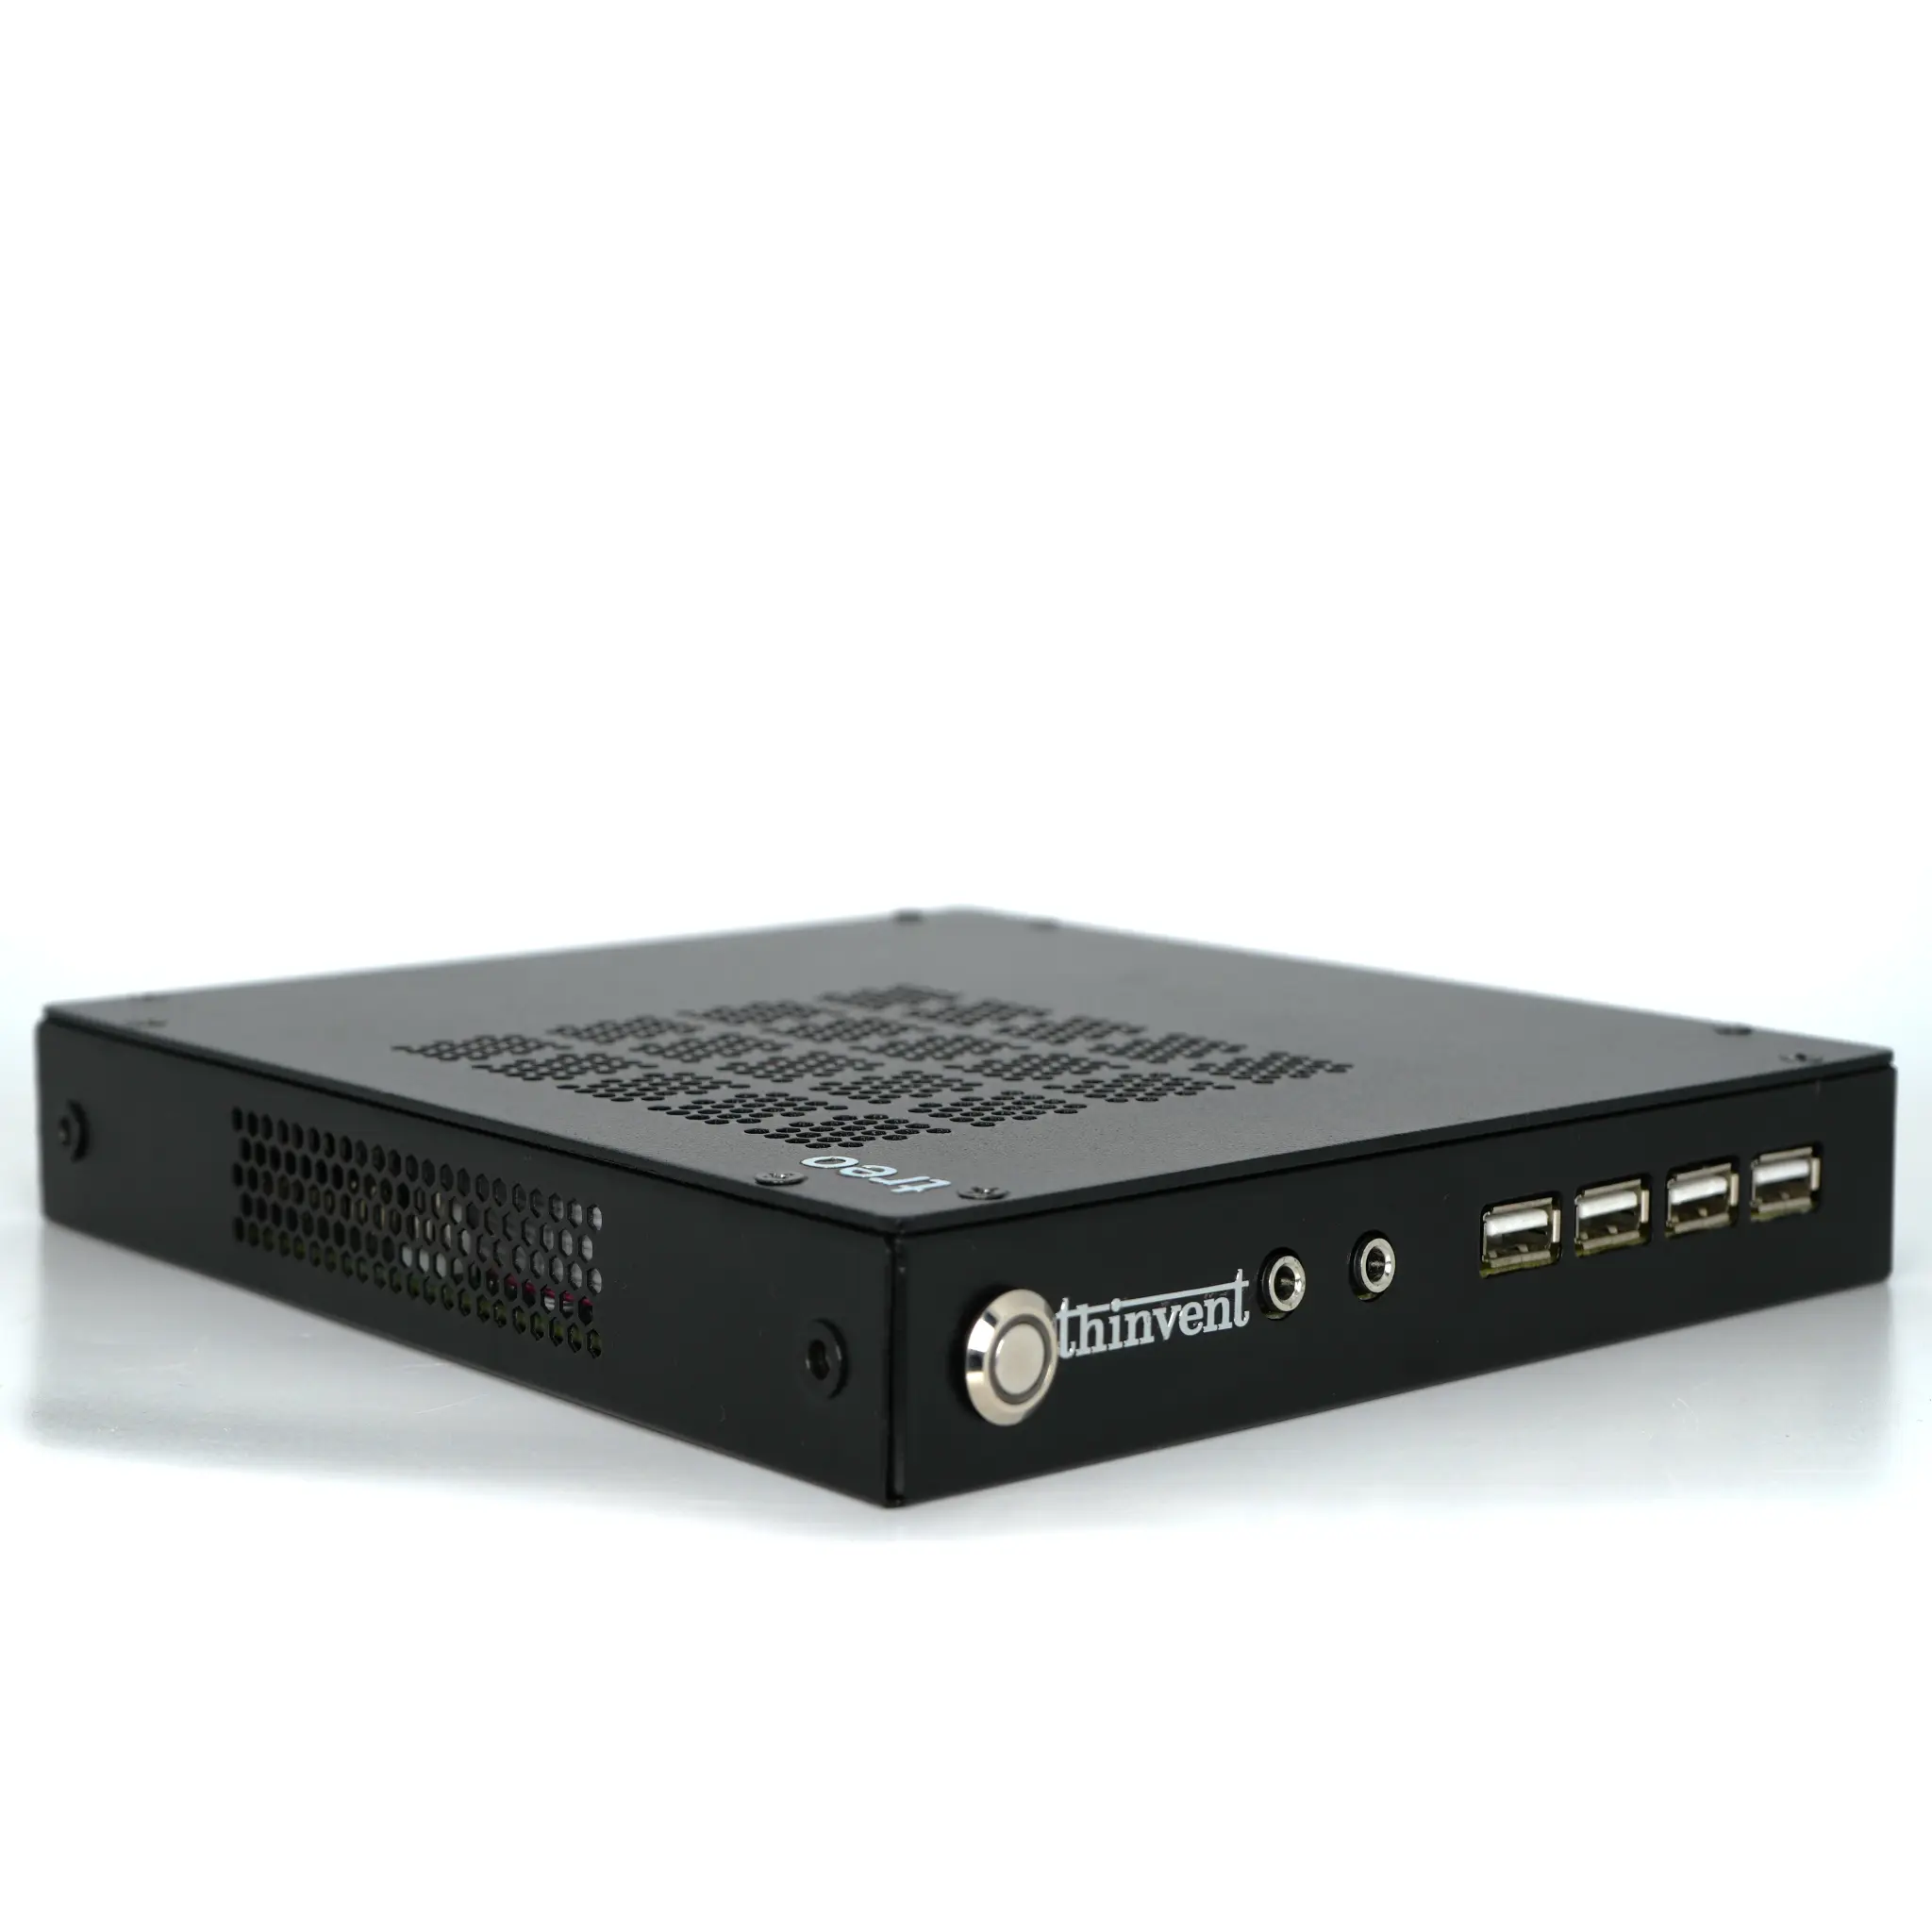
Industrial machinery manufacturing companies build, integrate and service the equipment that produces everything from automotive parts to packaged food, and almost every machine on a modern factory floor depends on a small industrial computer to run it. These companies need computing hardware that can sit inside or beside a machine tool, press, conveyor, extruder or packaging line and keep working for years in heat, dust, vibration and electrical noise. The typical requirement is a fanless industrial PC with wide-temperature operation, multiple serial ports for legacy controllers, dual Gigabit Ethernet for control and plant networks, and a long-life operating system image that can be locked down and deployed identically across hundreds of units.
What Industrial Machinery Manufacturers Use Industrial Computers For
Machine builders embed computers in three main places. The first is the machine control and HMI layer, where a panel-mount or DIN-rail PC runs the operator interface, recipe handling and motion or PLC supervisory logic. The second is the data acquisition and gateway layer, where an industrial PC collects Modbus, CAN, RS-232/RS-485 and OPC UA data from drives, sensors and older controllers, then forwards it to SCADA, MES or a cloud historian. The third is the quality and inspection layer, where vision systems, barcode and traceability stations, torque-tool controllers and laser marking systems need a stable, x86 platform with real USB and Ethernet throughput rather than a consumer desktop.
Legacy connectivity is often the deciding factor. Many machine tools, weigh indicators, servo drives and PLCs still expose only a DB9 serial interface, so a machine builder may need four or more RS-232/RS-485 ports on a single box. Because these ports